Drive-In Racking for Produce Cold Storage – A Case Study
Solution at a Glance
A family-owned tomato producer was relying on floor stacking pallets of their fresh produce. The company partnered with REB to design a storage solution fit for their operational needs. By integrating drive-in racking into their facility, REB helped the company increase throughput by optimizing storage density and organization.
- Products Provided: Drive-In Racking System, Pallet Rack Protection
- Services Provided: Rack System Design, Permitting support, Installation
- Industry: Food and Beverage
- Location: San Diego, CA
- Number of Projects REB has Completed for Customer: 1
Concern: Inefficient Storage Plan with Limitations and Safety Concerns
For years, a wholesale tomato producer stored palletized inventory directly on their cooler floor, stacking them multiple pallets high. While this may be the most cost-effective way to store inventory, it limits the amount of product that can be stored within the cooler by preventing the company from fully utilizing the building’s vertical space.
The pallets measure 40 inches wide by 48 inches deep by 72 inches high, weighing up to 1,800 pounds. Stacking these heavy pallets directly on top of one another occasionally resulted in damaged product. This also was making inventory more difficult to organize and retrieve.
As the company continued to see the drawbacks of storing their products like this, they sought a storage solution that would increase storage capacity, improve product safety, and organize their refrigerated area.
Solution: High-Density Drive-In Racking System for Produce Storage
High-Density Drive-In Rack Design
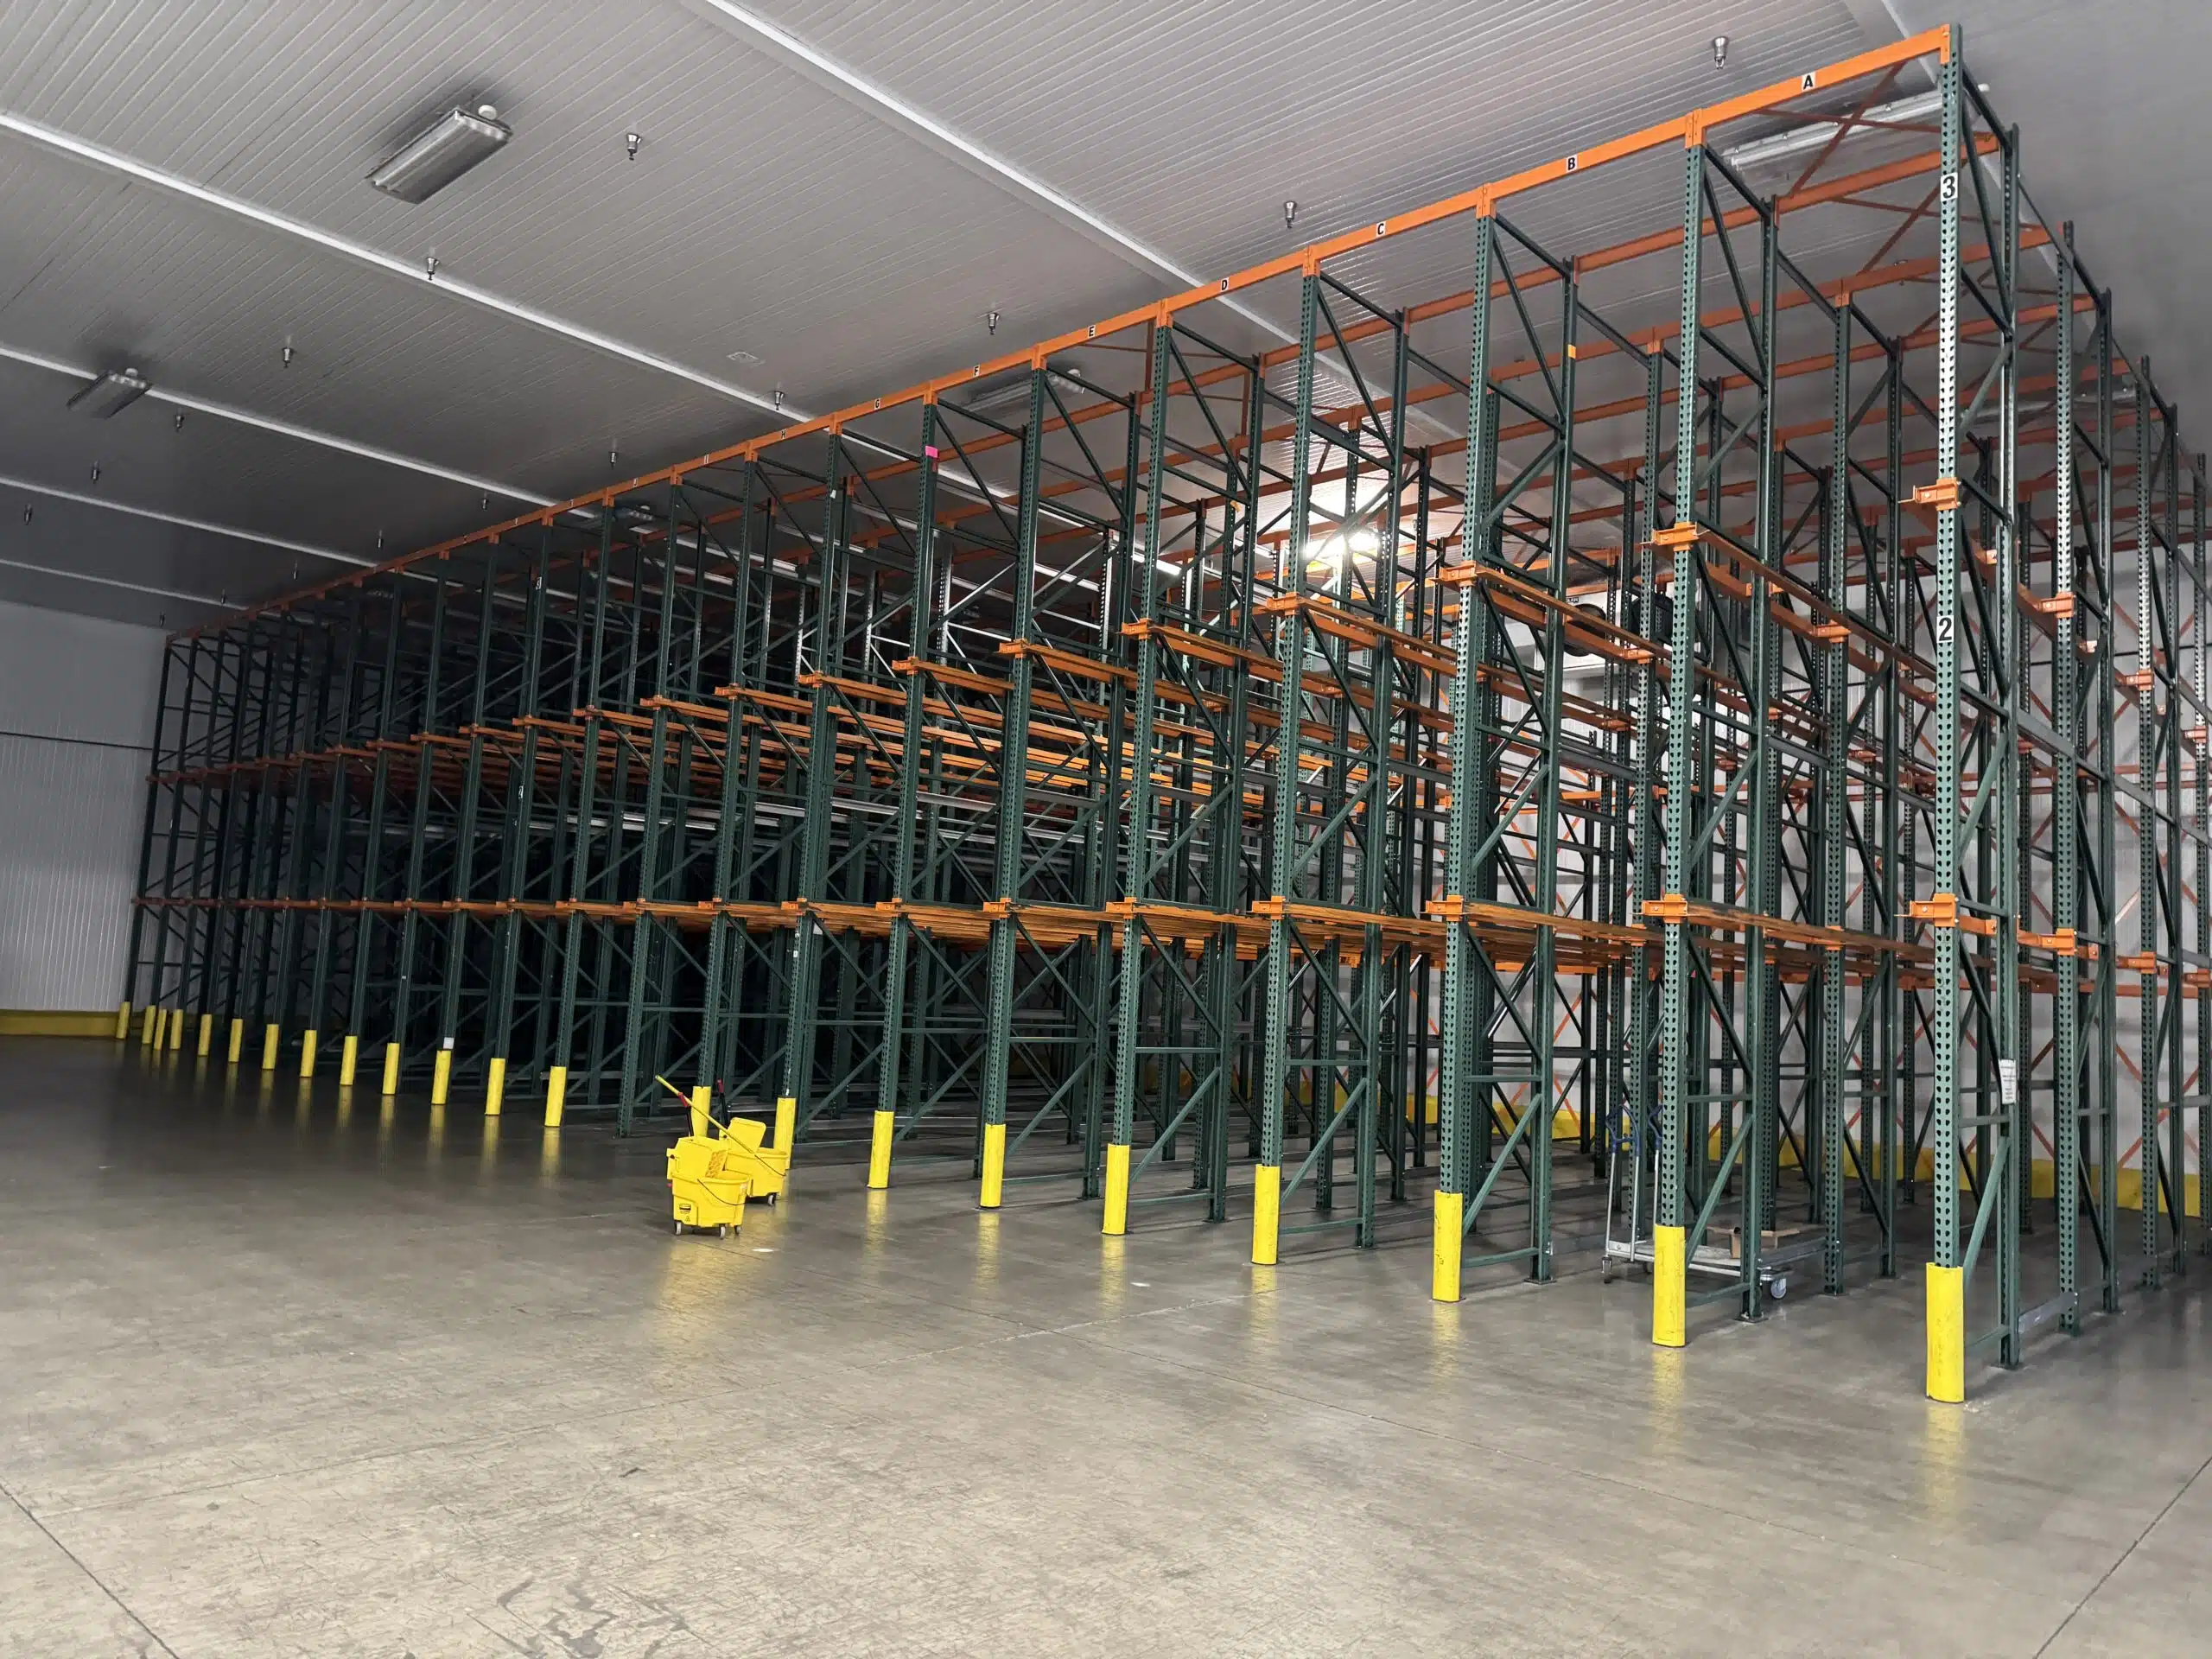
REB proposed a drive-in racking system based on the company’s storage and throughput requirements. Although the products are perishable, they are distributed in large, one-time shipments, eliminating the need to rotate inventory on a first-in, first-out (FIFO) basis. This allowed the company to prioritize storage density with a last-in, first-out (LIFO) drive-in system, which requires only one aisle for loading and unloading rather than the two aisles typically required for FIFO-compatible rack systems.
With a drive-in racking system, pallets of the same SKU can be loaded into the same drive-in lane. This makes shipping out many pallets of the same SKU more efficient. This system significantly increases storage density compared to conventional selective pallet rack. It also is an ideal solution for refrigerated facilities where optimizing the available floorspace is very important.
REB designed the system to fit the customer’s pallet dimensions while also accommodating for future growth. Each pallet position was designed to store loads up to 82 inches high and 2,000 pounds, allowing the facility to handle taller and heavier pallets if requirements changed.
Phased Installation to Support Future Growth
Rather than installing the entire system at once, REB designed a phased installation that aligned with the projected growth of their business.
This phased approach minimized upfront capital investment while ensuring the warehouse could expand without redesigning the overall storage layout.
Phase One: Immediate Storage Capacity Improvements
The first phase started in 2016. This phase included a new drive-in pallet rack system consisting of:
- 21 lanes of storage
- 3 pallet levels per lane
- 8 pallets deep
- 24 pallet positions per lane
- 504 total pallet positions
This configuration increases storage capacity and density by utilizing the building’s vertical space while also putting the inventory into clearly defined lanes.
Replacing floor stacking with engineered pallet rack also improves product handling by giving each pallet its own supported storage position.

Phase Two: Storage Expansion for Continued Growth
The second phase is designed to seamlessly extend the system installed in the first phase.
The expansion consists of:
- 19 additional storage lanes
- Three pallet levels high
- Eight pallets deep
- 24 pallet positions per lane
- 432 additional pallet positions
Upon completion of both phases, this system provides the company with 936 total pallet positions of storage.
Cold Storage Design Considerations
Maintaining consistent airflow helps support temperature uniformity, an important consideration for fresh produce storage where product quality depends on maintaining appropriate environmental conditions.
To maintain proper airflow throughout the cooler, REB designed the racking so that cooler fans remained unobstructed. Lanes that aligned with fan locations were modified by eliminating the upper pallet position closest to the fans, allowing the air to circulate more easily and effectively throughout the room.
Safety Features and Rack Protection
To help ensure that the system met local regulations and was code compliant, REB arranged for fire consultants to assess if the system met compliance codes and for sprinkler inspections.
Since the system requires the use of a forklift to pick and place the pallets, REB also incorporated upright protection into the system. Upright protection minimizes damage caused by forklift impacts and reduces the risk of structural damage to the system, helping to extend the lifespan of the storage system.
Project Management
In addition to procuring the pallet rack, REB managed several key aspects of the project to ensure the installation met all requirements.
Project responsibilities included:
- Rack system design
- Phased expansion planning
- Permitting support
- Fire safety coordination
- Installation management
By managing every aspect of the project, REB delivered a storage solution that provides the customer with exactly what they need, all with only needing one point of contact.
Outcome: Improved Storage Capacity and Operational Efficiency
The completed drive-in pallet racking system transformed how the tomato producer stored and handled palletized inventory within its refrigerated warehouse.
More Storage in the Existing Cooler Footprint
The 3-high, 8-deep drive-in configuration allows the company to take advantage of vertical space that was previously unused with floor-stacked inventory. By minimizing the number of aisles required for access, the system dedicates more of the cooler’s footprint to actual product storage, increasing density in a space where every square foot matters.
More Organized Inventory for Faster Handling
The combination of organized inventory and high-density drive-in storage makes pallet handling more efficient. Forklift operators can quickly identify and access the appropriate storage lane, while the drive-in configuration supports efficient movement of multiple pallets of the same SKU. This helps the company move product through the cooler and prepare large-volume shipments more efficiently.
Better Asset Protection
Moving pallets off the cooler floor and into dedicated rack positions provides greater control over how inventory is stored and retrieved. Instead of stacking heavy pallets directly on top of one another, each pallet is supported within the rack system, reducing the potential for product damage while making individual loads easier to locate and access.
Additionally, the incorporation of upright protection protects their rack system investment, and the inventory stored on it, from potential forklift collisions.
A Scalable Solution for Future Expansion
The phased approach allowed the company to improve its storage capacity without making the full investment upfront. Because the second phase was planned as an extension of the original system, the company can add capacity as its storage needs grow without having to completely redesign its cooler or replace the initial rack system.
Planning a High-Density Cold Storage Warehouse?
If you need a high-density storage solution, REB Storage Systems provides the design, permitting support, and installation expertise to optimize your available space.
Contact REB to discuss your storage requirements and develop a storage solution tailored to your products, facility, and operational goals.
We’d appreciate the opportunity to help you further, whether that be more information or a quote. Fill out the contact form on this page or call us at (800) 252-5955 to get in touch with a REB representative.
Share this post:
Submit Your Inquiry
Since 1962
REB has completed more than 100,000 projects in 15 countries (including all 50 states) for more than 20,000 customers across 50 industries, with 70% of customers as repeat buyers.
This is made possible by our team that has more than 300 years of industry experience designing and project managing material handling systems.
Learn more about REB's award winning service.