Selective and Carton Flow for Rack Supported Freezer and Dry Goods – A Case Study
Case Study Author: Philip Nelson
Solution at a Glance
Learn how a nationwide pet supply distributor needed a new distribution center capable of supporting both frozen and dry goods inventory. REB designed and implemented a rack supported freezer, selective pallet racking for dry goods, and carton flow racking to provide dedicated storage for different inventory requirements to support high density, efficient product picking, and quick movement throughout the facility.
- Products: Rack Supported Freezer, Selective Pallet Racking, Carton Flow Racking, Rack Protection
- Services: Design, Permitting Support, Installation, Project Management
- Industry: Pet Supplies Distribution
- Location: Geneva, IL
- Number of Projects REB has Completed for Customer: 1
Concern: New Distribution Center Required Multiple Storage Environments
A nationwide pet supplies distributor was expanding their operations and needed a new distribution center that required room temperature and cold storage capabilities. The company found a 270,000-square-foot warehouse that could support its expansion, but the facility needed to be configured to accommodate the different storage and material handling requirements of its products.
The customer also needed the freezer construction and racking installation to work together as part of the overall facility buildout. Rather than treating the freezer and its racking as sequential projects, the construction and installation needed to happen concurrently.
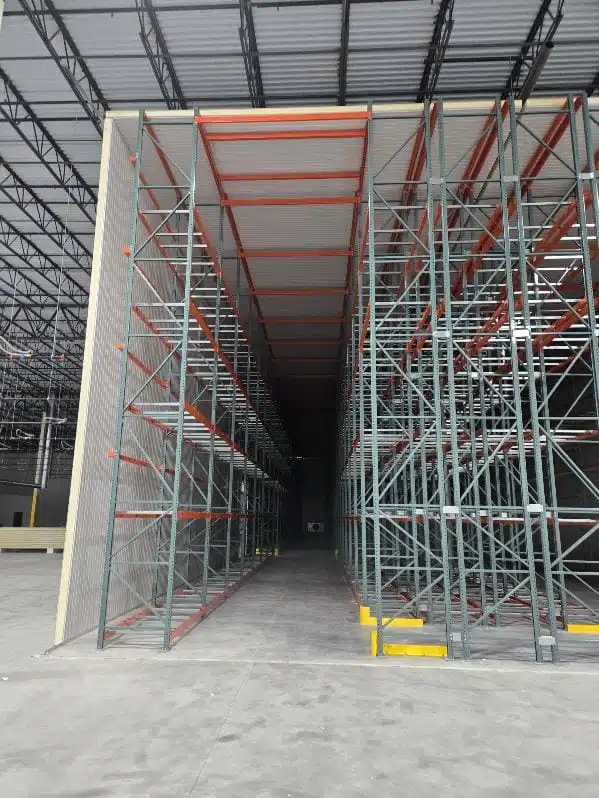
Solution: Rack Supported Freezer for Maximum Cold Storage Within the Facility
Instead of constructing a separate freezer structure and then installing racking inside it, the customer chose a rack supported freezer. In this type of construction, the pallet rack serves as the primary structural support for the freezer walls and roof. Because the rack is integrated into the structure, the design eliminates the need for separate building frameworks and structural columns within the storage area, which allows more of the available footprint and vertical space to be dedicated to pallet storage.
The rack supported approach allowed the freezer and storage system to be designed together rather than treating the freezer enclosure and racking as independent components. Having them designed as one structure expedited permitting approvals for some elements and therefore decreased construction time.
REB worked with the supplier of the cold storage equipment to design the racking so that it meets the freezer paneling’s requirements and support the freezer coils properly. The installation teams for both the racking and the enclosure worked concurrently to ensure that the installation was completed efficiently and properly.
In total, the rack supported freezer provides the company with 138 bays of racking and a total of 1,296 pallet positions.
Solution: Selective Rack for High Selectivity of Dry Goods
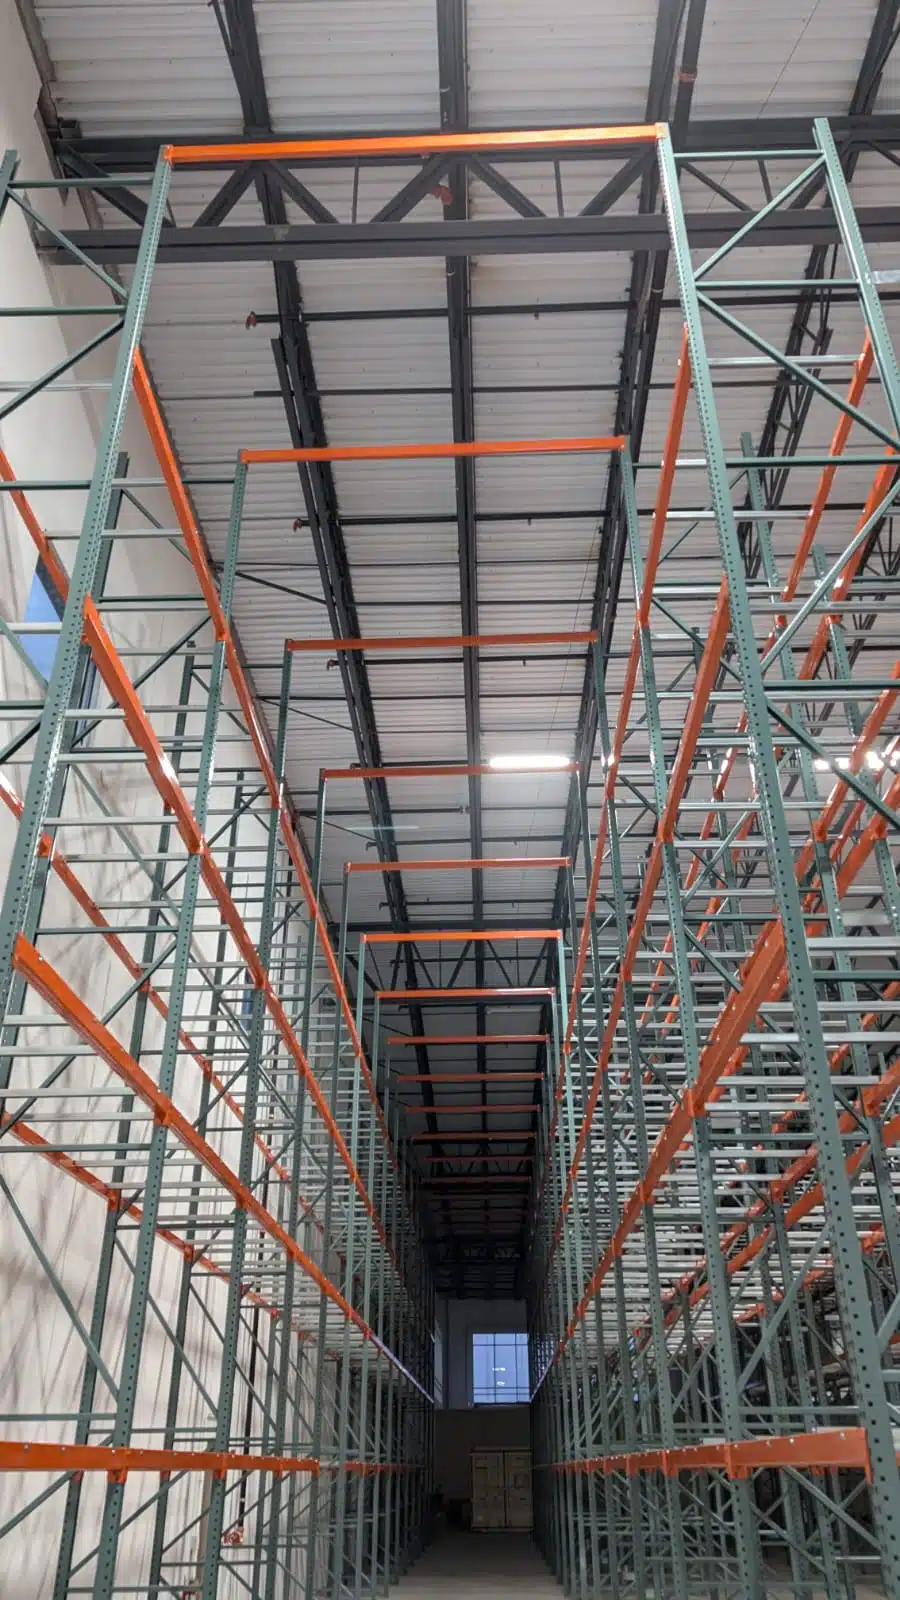
For the dry goods that the company needs to store in the facility, REB proposed 5-high standard selective racking. Selective rack provides direct access to individual pallets, making it appropriate for inventory that requires accessibility rather than the higher density and lower selectivity associated with systems such as drive-in rack.
The 5-high design also allows the company to better utilize the vertical space within the warehouse, reducing the need for more lateral storage space.
In total, the dry goods racking provides the company with 105 bays of racking and a total of 1,046 pallet positions, giving the customer a dedicated reserve storage area designed around the needs of its ambient inventory.
Solution: Carton Flow Rack for Efficient Packing Operation
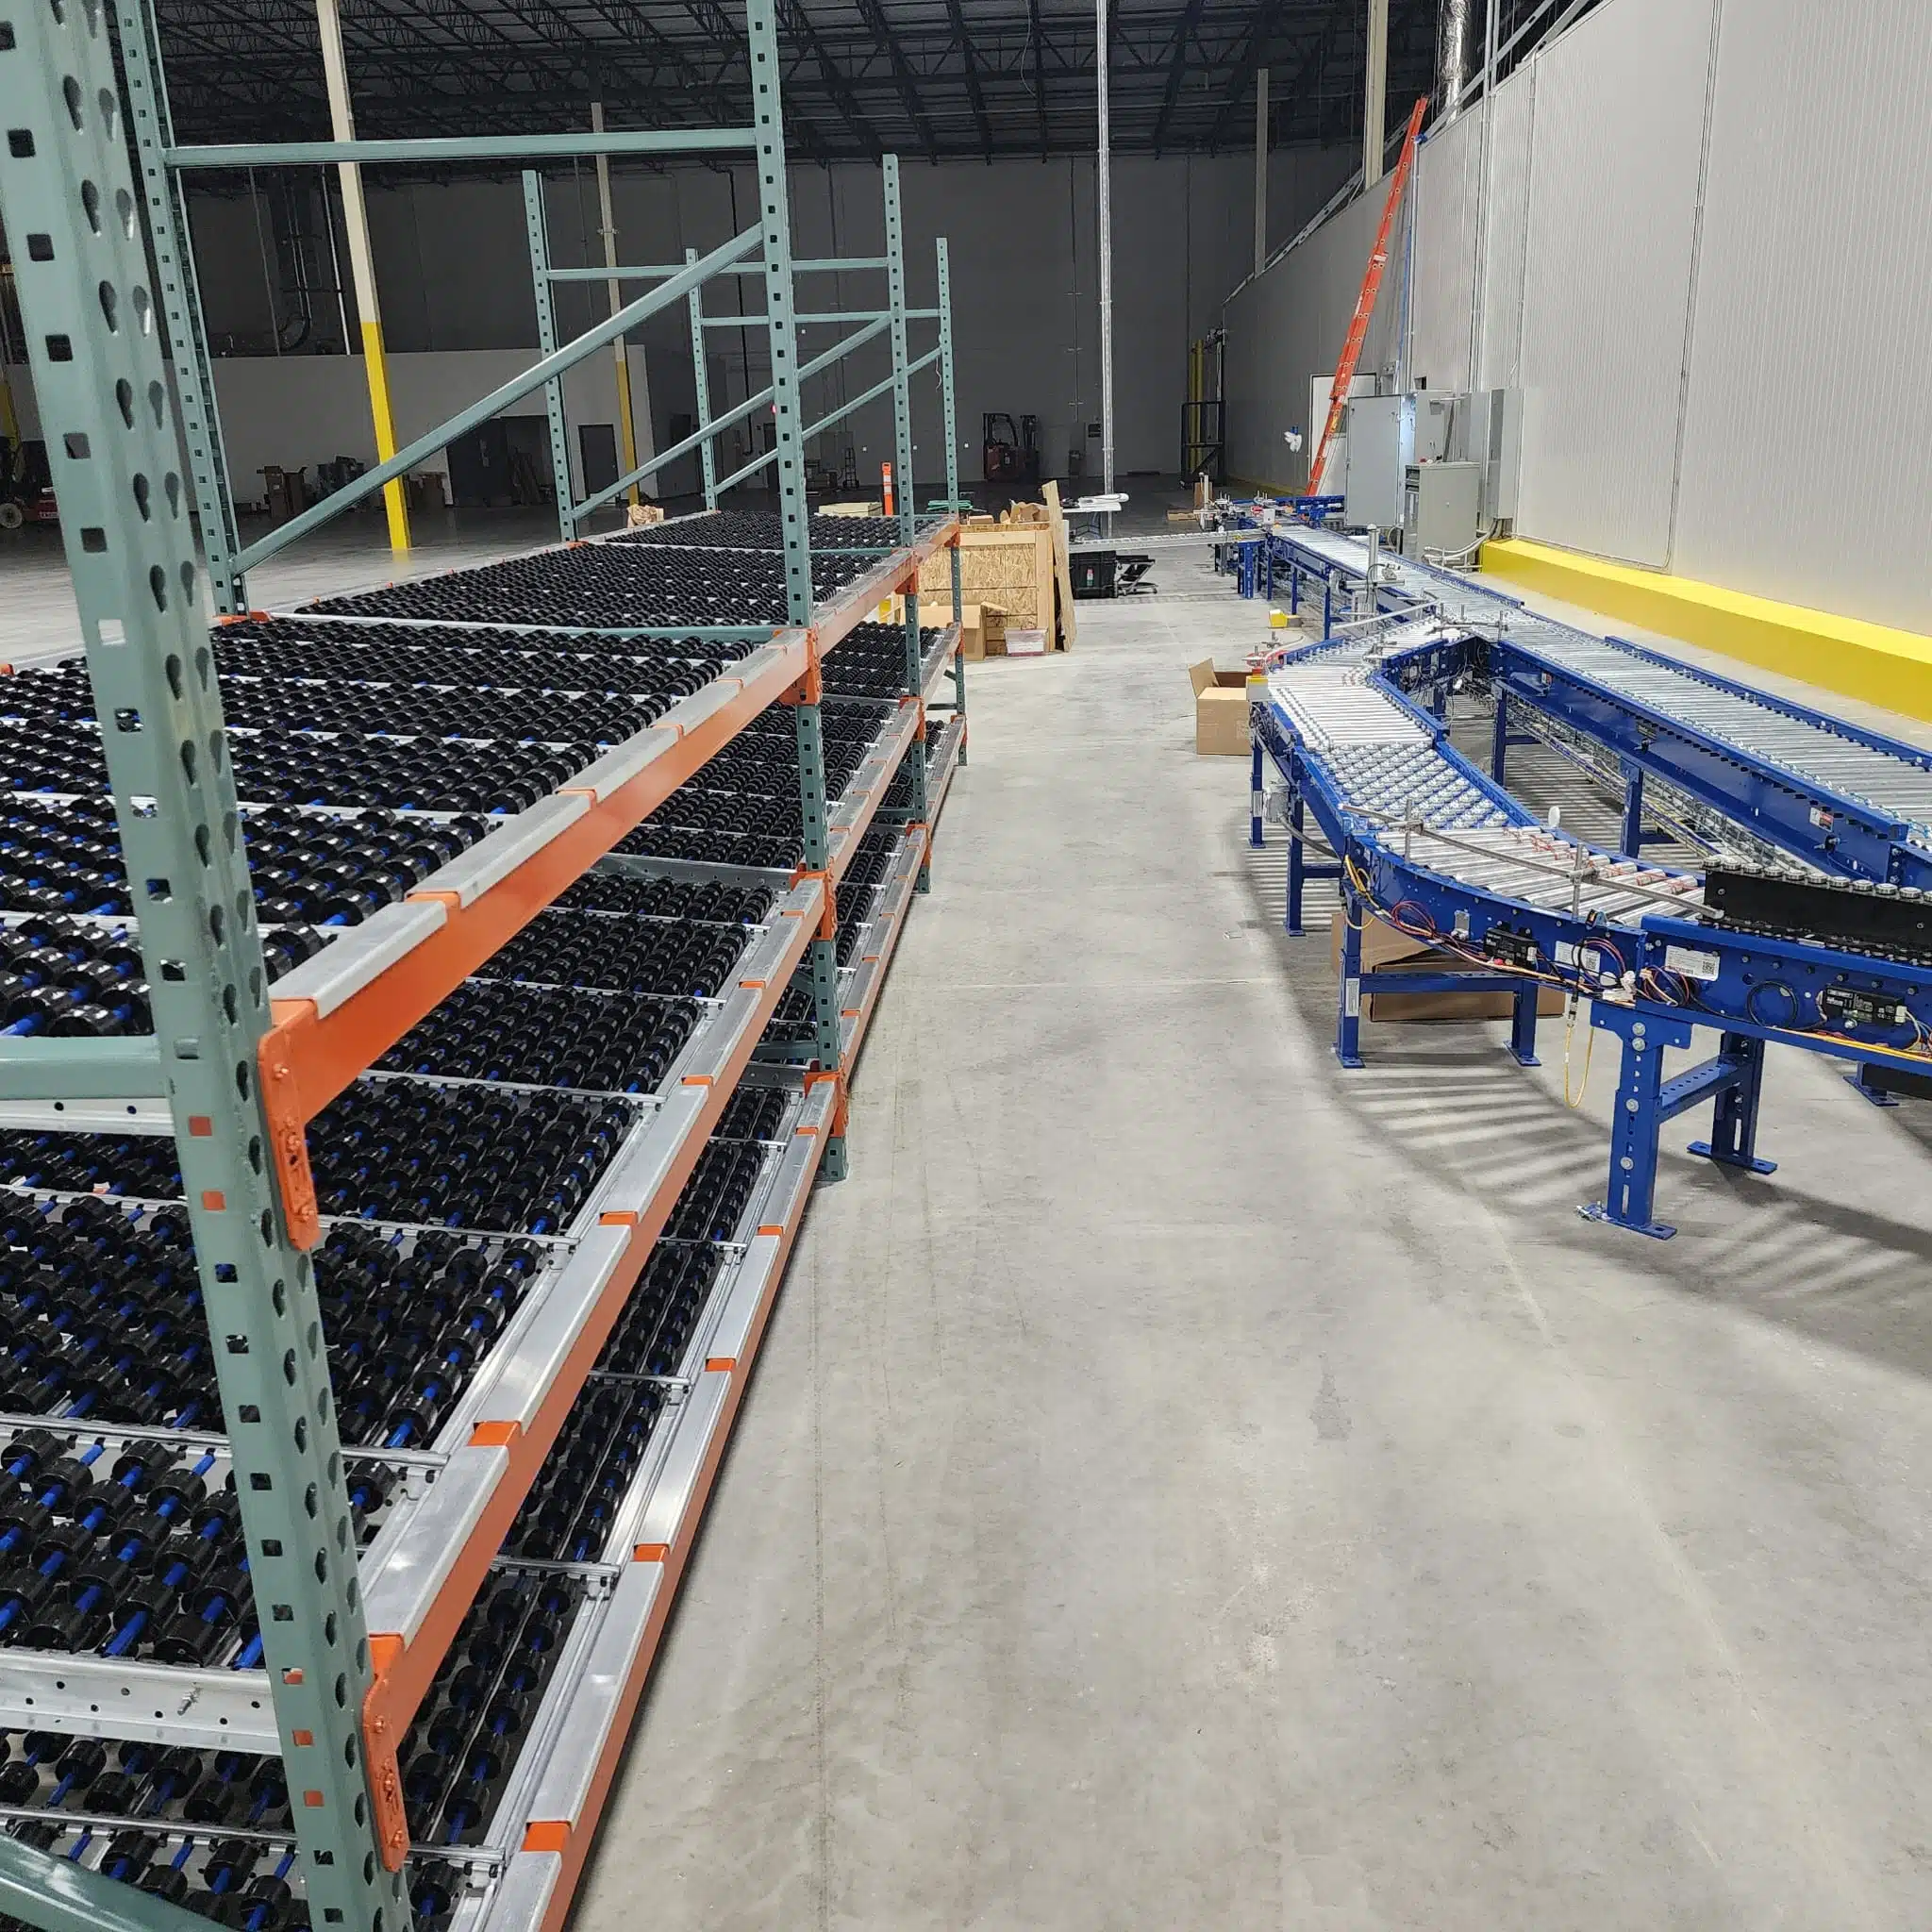
The company was also having conveyor installed, by a third party, into their facility to help with the packing and shipping process. To assist in the overall flow of this solution, REB proposed carton flow racking. The racking supplements the conveyor by providing a high-throughput solution that could be used for picking and packing boxes. REB designed and installed 3 bays of carton flow based on the customer’s needs.
Carton flow uses inclined rollers to move stored items toward the picking face as product is removed. This allows inventory to be replenished from the rear while pickers access product from the front, making the system particularly useful for high-activity picking applications.
For this customer, the carton flow system supports the conveyor by providing a high-throughput solution for picking and packing boxes. REB designed and installed 3 bays of carton flow based on the customer’s needs.
Outcome: Coordinated Storage Solutions Optimize Space and Increase Throughput for Multiple Storage Environments
The coordinated design and implementation of the selective racking used in the ambient storage area, the rack supported freezer, and the carton flow racking has provided the pet food distributor advantages in the construction of their material handling system as well as improvements in their overall operations.
Integrated Storage Systems for Different Operational Requirements
The combination of rack types allows the customer to address three different operational needs within one facility: high-capacity frozen pallet storage, accessible dry goods storage, and efficient case picking. Designing these systems together gave the customer a storage solution tailored to how products move through their distribution center.
Maximized Cold Storage Capacity
By installing a rack supported freezer, the company designed their cold storage in a space that was optimized to perfectly fit the storage requirements they have.
The rack supported freezer allows the customer to incorporate a dedicated frozen storage environment while using the racking itself as the structural support for the enclosure. With fewer structural obstructions within the freezer, more of the available space can be used for pallet storage, resulting in 1,296 pallet positions across 138 bays.
High Selectivity of Dry Goods Storage
The selective rack configuration gives the customer direct access to individual pallets of dry goods. This system allows inventory to be stored vertically while maintaining the accessibility needed for an active distribution environment.
Efficient Packing Operation
Carton flow provides a dedicated packing station and helps keep product moving toward the pick face as supplies are removed so that they are automatically ready for the packer.
Reduced Costs for Construction and Real Estate
Having the racking and freezer install teams working concurrently helped reduce costs by ensuring that the installation of the racking was being done correctly given the freezer’s requirements.
Additionally, constructing a rack supported freezer within an existing ambient warehouse allows the company to keep both dry and cold storage in one location instead of having a separate facility to handle their cold storage needs.
Maximized Storage Capacity
The absence of building columns within the freezer increases usable storage space, allowing for a higher number of pallet positions and full use of the space within the freezer. Also, the use of vertical warehouse space helps the company achieve the highest storage capacity possible.
Faster Construction
The concurrent installation of the racking and the freezer components resulted in quicker job completion compared to consecutive construction of these systems.
Contact REB for Your Rack Supported Cooler or Warehouse Storage Requirement
At REB Storage Systems International, we look at each project as unique. While many have similarities for which we can leverage our experience and knowledge, each client has unique needs that must be met.
REB has the flexibility to integrate products from multiple manufacturers based on the requirements of your rack system including pricing and lead time. This combined with in-house design, project management, and permitting support allows us to provide you with your unique storage solution.
To receive a storage solution that optimizes your unique requirements, fill in the contact form on this page or call (800) 252-5955.
About the Author
Philip Nelson is REB’s Vice President of Sales & Business Development. Since joining REB in 2016, Phil has held progressively senior sales leadership positions while helping customers implement projects ranging from conventional pallet racking systems to complex multi-level storage and automation solutions. His experience includes developing custom storage concepts, coordinating national account programs, managing vendor relationships, and supporting customers through every stage of the decision-making process.
Phil is an active member in the material handling industry. He has hosted presentations for Modern Materials Handling, has attended/exhibited at MODEX, ProMat, and MHEDA conferences, and is an active participant in other educational events and training programs in the industry.
You can learn more about Phil Nelson and the projects he has worked on by visiting his profile.
More Case Studies and Articles Related to Cold Storage Systems
Articles:
- Cold Storage Racking 101: Picking the Right Cold Storage Racks
- Rack Supported Building: Benefits & Ideal Applications | REB
- Keg Storage: Optimizing & Choosing A Keg Storage System | REB
- Why A Rack Supported Cooler or Freezer is Ideal For Your Operation | REB Storage Systems
Case Studies:
- Rack Supported Cooler and Freezer – A Case Study | REB Storage Systems
- Selective + Push Back for Dry, Cooler, and Freezer Storage
- Rack Safety Inspections + Rack Repair Kits for Food and Beverage Cold Storage – A Case Study | REB Storage Systems
- Drive-In Racking for Produce Cold Storage – A Case Study | REB Storage Systems
Share this post:
Submit Your Inquiry
Since 1962
REB has completed more than 100,000 projects in 15 countries (including all 50 states) for more than 20,000 customers across 50 industries, with 70% of customers as repeat buyers.
This is made possible by our team that has more than 300 years of industry experience designing and project managing material handling systems.
Learn more about REB's award winning service.